
special.elbow.production. — Bünde, Germany
Pipe bends direct from the manufacturer – Siekmann
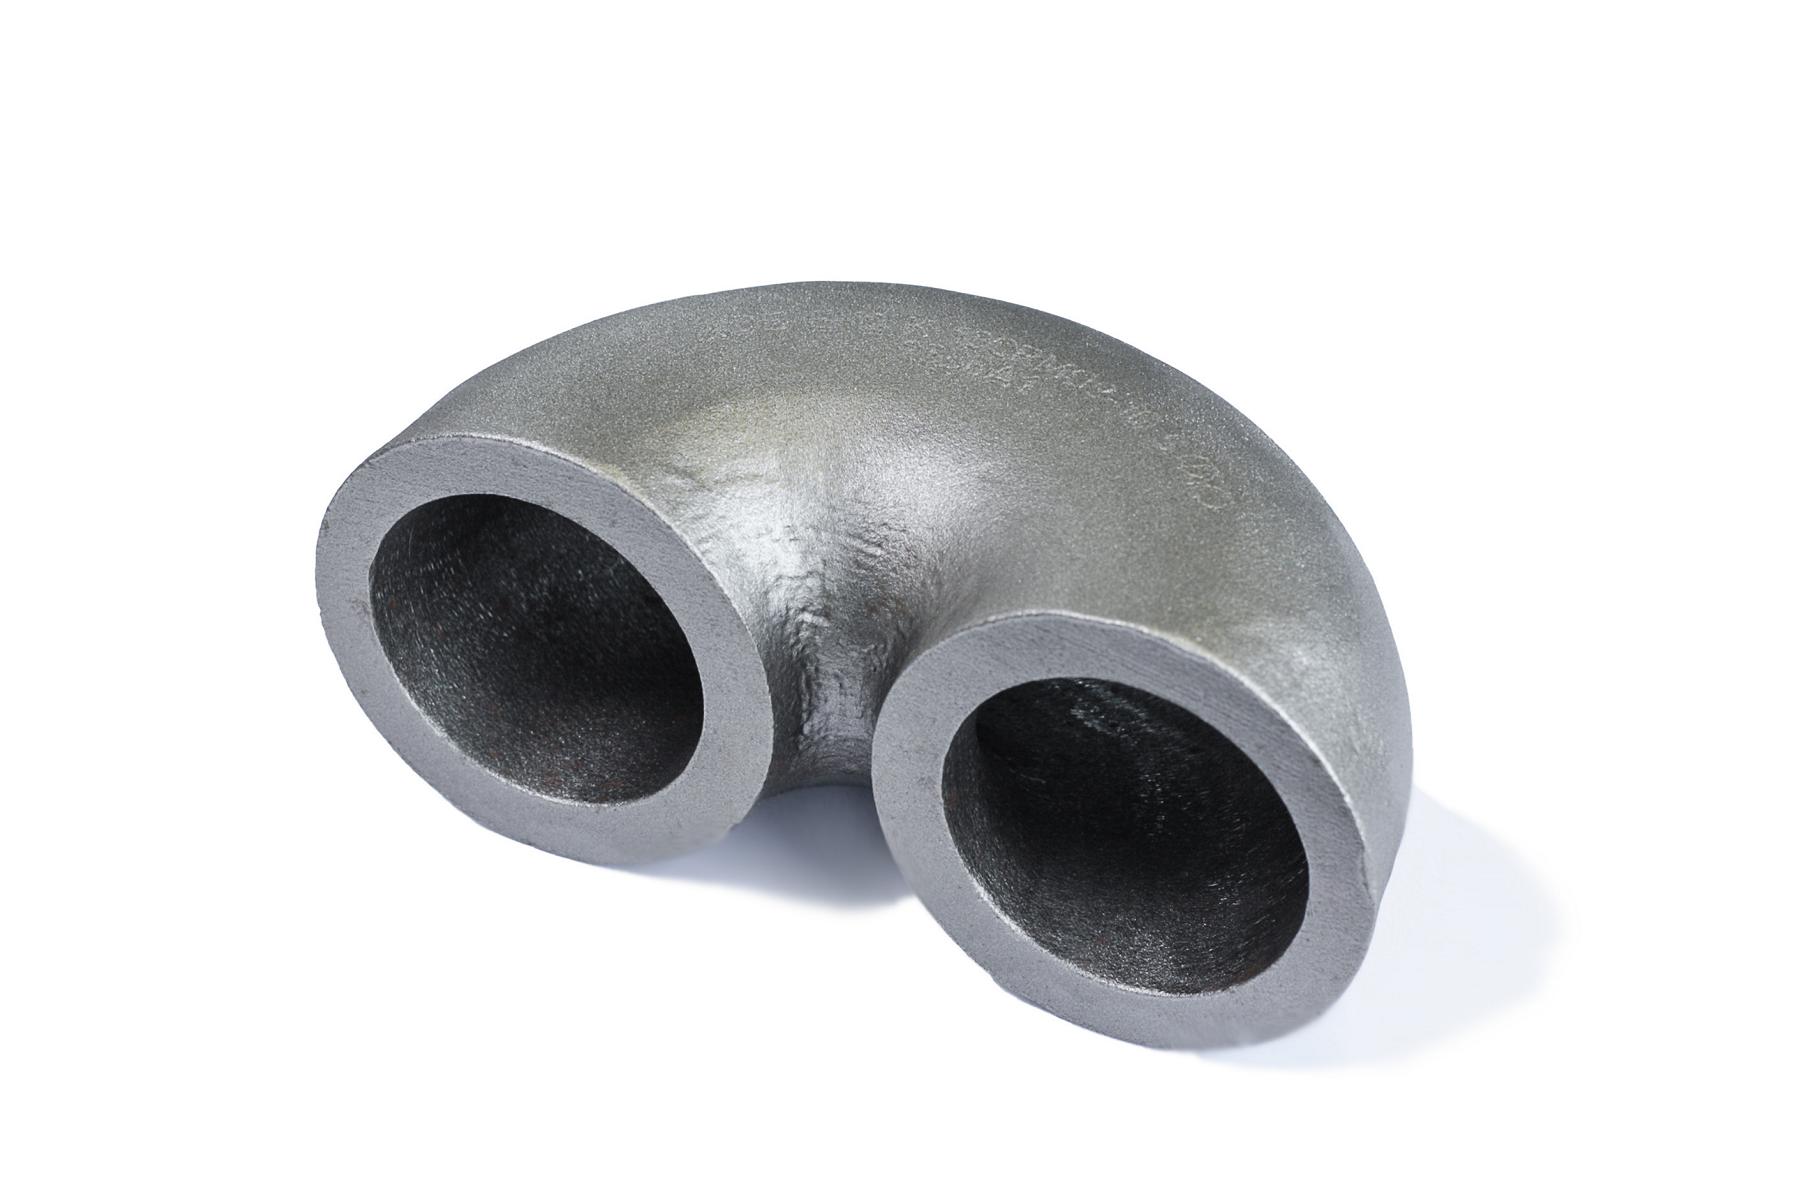
Seamless, heavy-wall special pipe bends in carbon steel and stainless steel. Manufactured to EN 10253, DIN 2605 and ASME B16.9.
- EN 10253
- DIN 2605
- ASME B16.9
- ISO 9001:2015 · TÜV Nord

- Outside diameter
- 13.7 – 219.1 mm
- Wall thickness
- 1 – 55 mm
- Bending radius tolerance
- down to ±1 mm
- Certified
- ISO 9001:2015 · TÜV Nord
 Product range
Seamless. Heavy-wall. Even in small batches.
Siekmann GmbH & Co. KG is your reliable partner for pipe bends made from seamless pipe – manufactured in Germany.
We process carbon steel and stainless steel and specialise in heavy-wall butt-weld pipe bends and special pipe bends. Our strength is precise forming – even for small quantities and short delivery times. As a manufacturer we keep our own stock of blanks, so we can deliver single items at short notice.
Our product range at a glance
- Seamless pipe bends with heavy wall thicknesses
- Special radii and pipe bends with tight tolerances
- Carbon steel, high-alloy materials and stainless steel
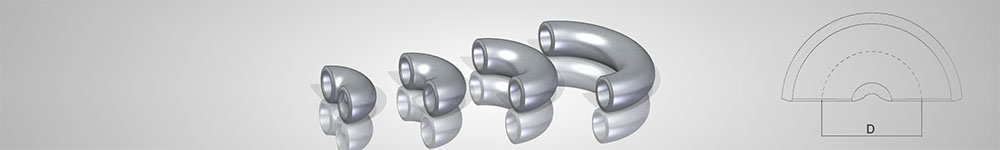
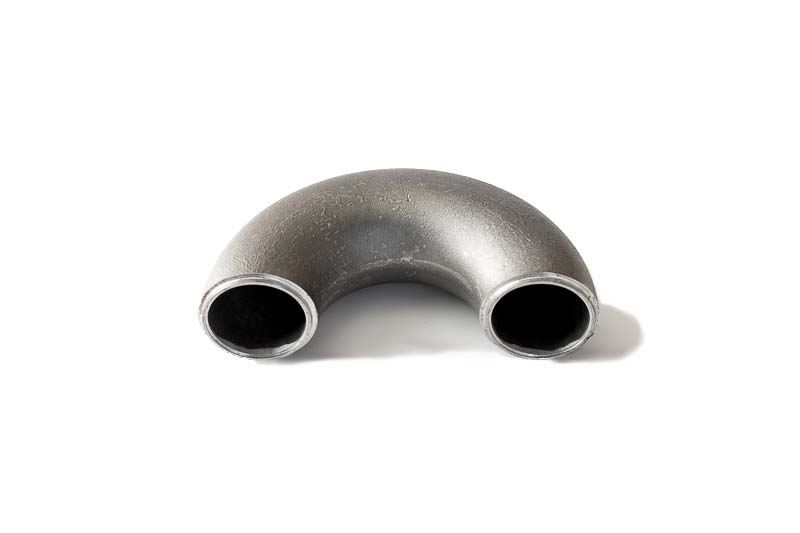
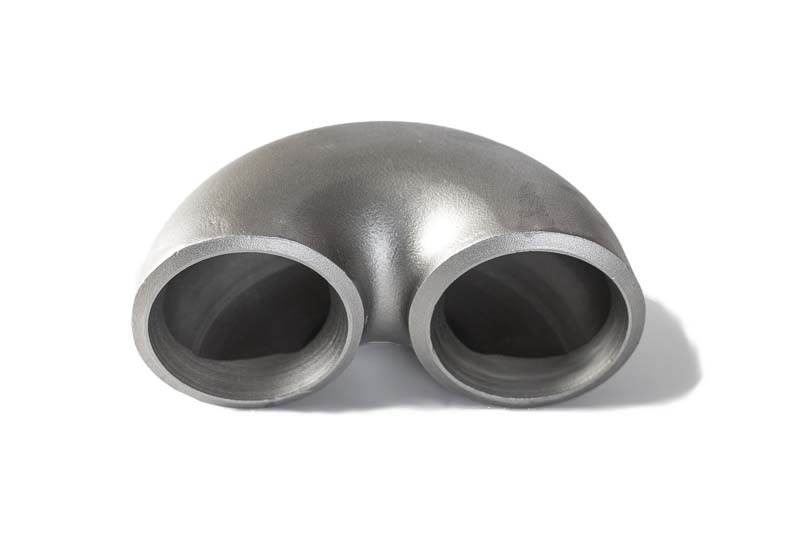
- 45°, 90° and 180° pipe bends – intermediate angles also possible
- Type B pipe bends to EN 10253-2, EN 10253-4 or DIN 2605 Part 2 with full pressure factor
- Small batches and single items with very short delivery times
We manufacture pipe bends to EN 10253, DIN 2605 or ASME B16.9:
| Outside diameter | 13.7 mm – 219.1 mm |
|---|---|
| Wall thickness | 1 mm to 55 mm, depending on outside diameter |
| Angle | 15°, 30°, 45°, 90°, 180° and intermediate angles, depending on size |
| Type | 2D, 3D, 5D, Long Radius (LR), Short Radius (SR) – more radii under Bending radii |
| Standards | EN 10253 Type A and B, DIN 2605 Part 1 and 2, ASME B16.9, manufacture to customer specification |
| Tolerances | We manufacture to the usual tolerances of the pipe bend standards – often tighter, e.g. with a bending diameter tolerance of ±1 mm. |
Our pipe bends are used worldwide – for example in refineries and power plants, high-efficiency gas power plants, on oil platforms, in heat exchangers and in mechanical engineering.
We supply seamless pipe bends in carbon steel, high-alloy steel or stainless steel. Our extensive experience in heat treatment allows us to form a wide range of materials – see the list under Materials.
Our production is subject to strict quality control: dimensional checks accompany every stage of manufacture, so deviations are detected early. Siekmann is monitored by TÜV Nord and certified to ISO 9001:2015 – the basis for continuous improvement of our processes. More under Service & quality.
Looking to buy pipe bends? Our contact page has a form for sending your request directly.
Send a request →Materials
Materials for pipe bends
Over the years we have gained broad experience in pipe bend manufacturing. Carbon steels, high-alloy steels and stainless steels are among the materials we process. We manufacture pipe bends from the following materials:
- P235GH TC1/2 (St 35.8 I/III)
- P265GH
- S355J2H
- 16Mo3 (15Mo3)
- 10CrMo9-10 (10CrMo910)
- 13CrMo4-5 (13CrMo44)
- X11CrMo5
- X11CrMo9-1
- X20CrMoV11-1
- X10CrMoVNb9-1
- X10CrWMoVNb9-2
- 7CrMoVTiB10-10
- P215NL (TTSt35N/V)
- 12Ni14 (10Ni14)
- P355N (StE355)
- P355NH (WStE355)
- P355NL1 (TStE355)
- P355NL2
- L290NB (StE 290.7)
- L360NB (StE 360.7)
- L415
- 1.4301
- 1.4306
- 1.4361
- 1.4362 (Lean Duplex)
- 1.4401
- 1.4404
- 1.4410
- 1.4435
- 1.4436
- 1.4439
- 1.4462 (Duplex)
- 1.4466 (Super Duplex)
- 1.4501
- 1.4539
- 1.4541
- 1.4547
- 1.4550
- 1.4571
- 1.4841
- 1.4749
- 1.4828
- 1.4878
- 1.4876
- 1.4952
- 1.4835
- 1.4877
- 1.4910
- 1.4922
- WPA
- WPB
- WPC
- WP1
- WP5
- WP9
- WP11
- WP12
- WP22
- WP32/27
- WP91
- WP92
- WP304
- WP304H
- WP304L
- WP310
- WP316
- WP316L
- WP316Ti
- WP321
- WP347
- WP347H
- WPL3
- WPL6
- X42
- X52
- WPHY52
- WPHY60
- S30815
- S31000
- S31050
- S31500
- S31726
- S31803
- S32760
- N08904
- Alloy 800H
- DMV310N
Your material is not listed? Ask us – thanks to our heat treatment experience we also form special materials.


Standards
Which standards apply to pipe bends?
Since July 2026, DIN EN 10253-2:2026-07 (EN 10253-2:2021+A1:2025) applies to ferritic steels, and since October 2025, DIN EN 10253-4:2025-10 applies to austenitic and duplex steels. Both editions contain bending radii that differ in part from the previous standards. We are happy to explain the differences – get in touch.
EN 10253-2
The current standard for butt-welding fittings made of non-alloy and alloy ferritic steels with specific inspection requirements. It combines several DIN standards for different fittings into one European standard; the pipe bend part is the relevant one for us. We supply types 2D, 3D, 5D and many special radii in between. The standard also covers pipe bends with full pressure factor (Type B): these have a significantly thicker wall on the inside of the bend, where stress is highest. Various options can also be agreed.
Example — Option 15: Each fitting shall be hardness tested.
EN 10253-4
This standard covers butt-welding fittings made of austenitic and austenitic-ferritic (duplex) steels with specific inspection requirements. It largely corresponds to EN 10253-2, but some bending radii differ. Our team is happy to explain the differences. The options of EN 10253-2 are also included here, but differ fundamentally.
Example — Option 15: An inspection certificate 3.2 to EN 10204 shall be issued.
DIN 2605
The former German pipe bend standard, now replaced by EN 10253. For pipe bends with full pressure factor it specifies different wall thicknesses than the new standards. DIN 2605 is less extensive than EN 10253 and covers only pipe bends, no other fittings.
ASME B16.9
ASME B16.9 sets out the technical requirements for seamless and welded steel fittings – including pipe bends in different designs. Dimensions are given in inches (outside diameter) and schedules (wall thicknesses). Pipe bends to ASME B16.9 are used worldwide in plant and pipeline construction and stand for high compatibility and compliance.
Basics
What is a pipe bend?
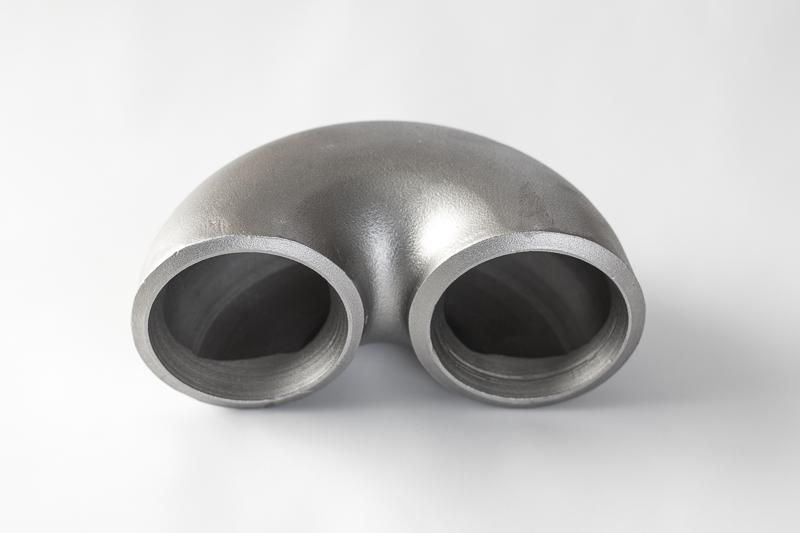
A pipe bend is a pipe fitting that changes the direction of a piping system. Pipe bends differ in outside diameter, wall thickness, bending radius, angle and material. They are usually made either from welded half-shells or – as at Siekmann – from seamless pipe. Pipe bends are used in power plant construction, mechanical engineering, heat exchanger and plant construction and many other fields.
Pressure factor
Type A / Type B – the difference
Type A – reduced pressure factor
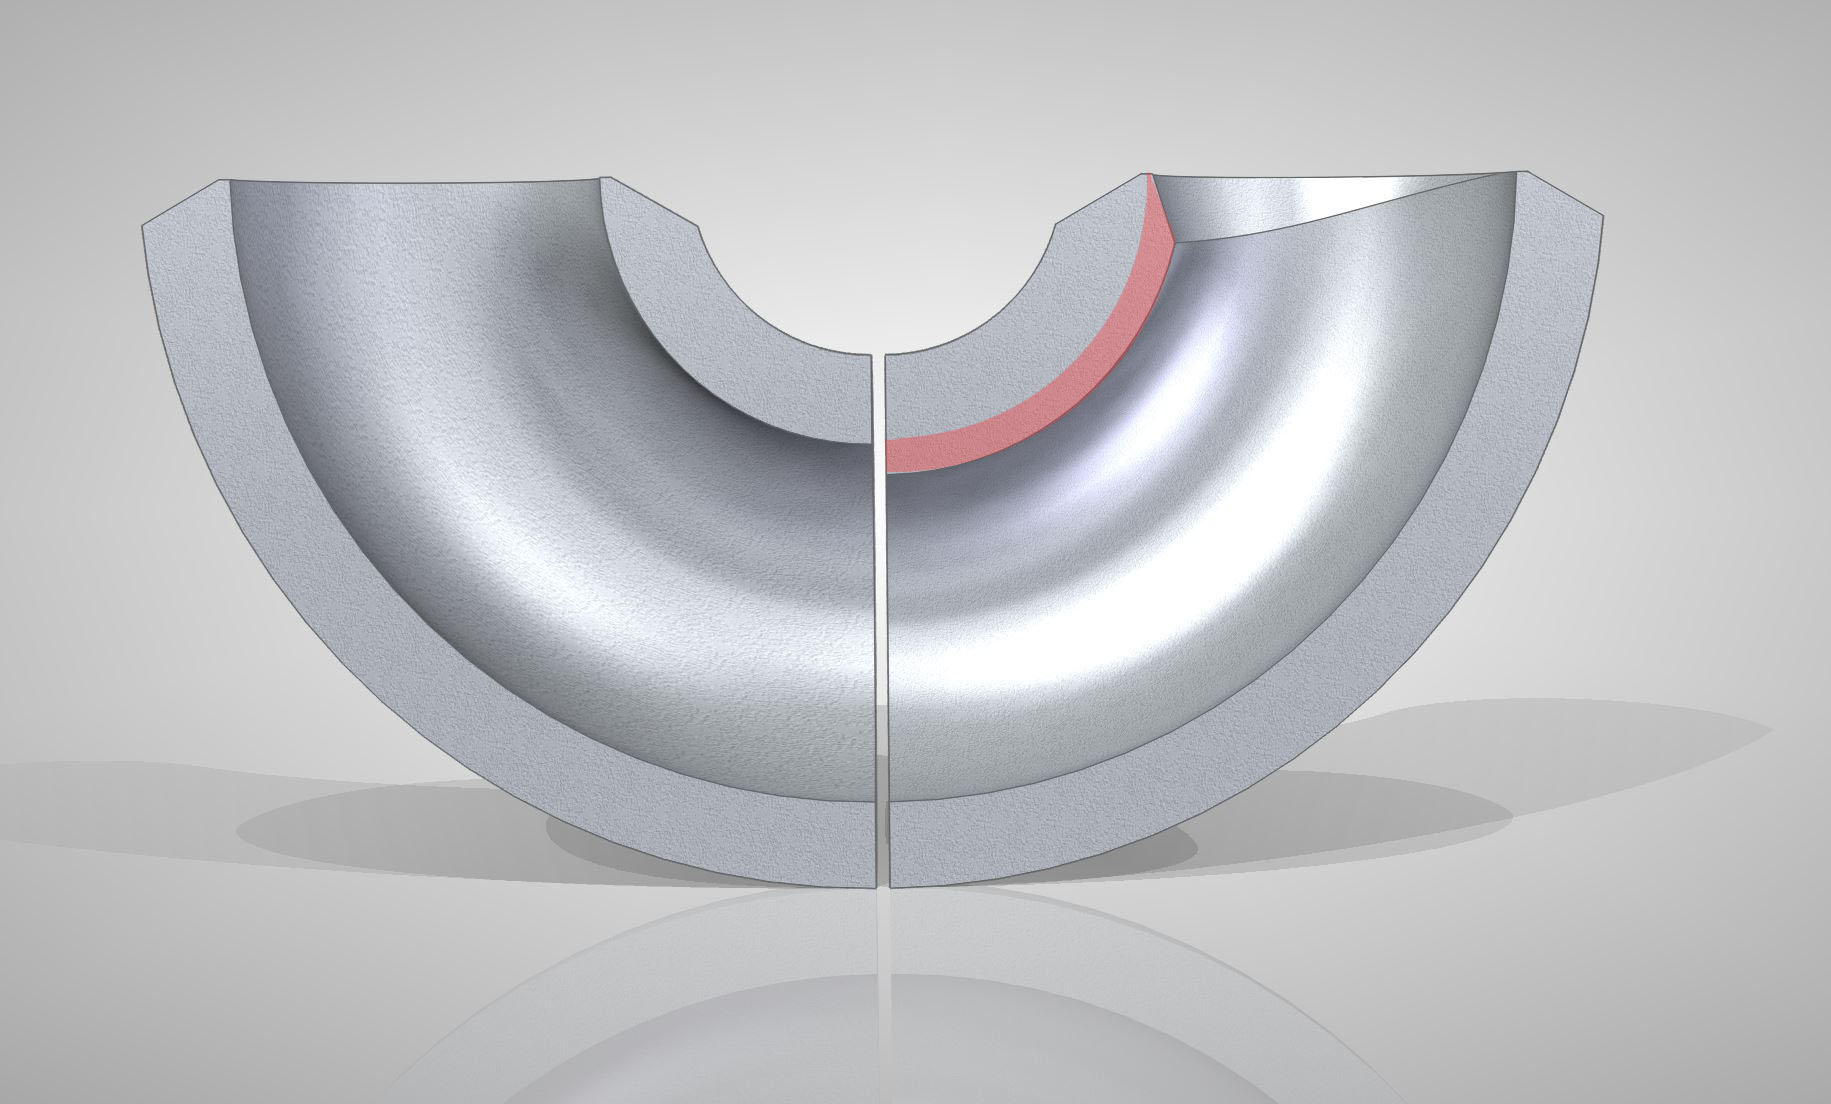
The fittings have the same wall thickness on the bend body as at the weld ends. Their resistance to internal pressure is lower than that of a pipe with the same outside diameter, wall thickness and material – hence the term reduced pressure factor. As at the pipe connection, the wall thickness over the whole fitting body must not fall below −12.5 % of the nominal wall thickness.
Example 76.1 × 12.5 (2D)Inner wall thickness: 11.0 mm
Type B – full pressure factor
The fittings have an increased wall thickness on the inside of the bend body. Their resistance to internal pressure equals that of a pipe with the same outside diameter, wall thickness and material – the full pressure factor. The required wall thickness on the inside of the bend is calculated with a complex formula from outside diameter, wall thickness and, above all, bending diameter. Pipe bends with particularly tight bending diameters need a much thicker inner wall.
Example 76.1 × 12.5 (2D)Inner wall thickness: 16.8 mm
EN 10253-2 and EN 10253-4 classify pipe bends into two types under different names: EN 10253-2 calls them Type A and Type B, EN 10253-4 calls them Design A and Design B.
Wall thickness calculator Type A / Type B
Enter the outside diameter and nominal wall thickness and move the bending radius. The bars show the minimum wall of a Type A bend (nominal wall −12.5 %) and the required minimum wall tint,min on the intrados of a Type B bend to EN 10253-2.
Values for guidance only, rounded up to 0.1 mm. They do not replace a design calculation.
Part 1 or Part 2 to DIN 2605
DIN 2605 also distinguishes between reduced and full pressure factor. With full pressure factor – the Part 2 pipe bend – the wall in the inner curve is considerably thicker. Unlike EN 10253, DIN 2605 does not give a calculation formula but lists the wall thicknesses in tables.
The Part 1 pipe bend has no reinforcement on the inner radius; the same wall thickness tolerances apply over the whole bend.
Types
Differences between pipe bend types
Pipe bends differ in outside diameter, wall thickness and bending diameter. The standards define so-called standard types for the bending diameter – this harmonisation helps designers with planning. EN and DIN define the standard types 2D, 3D, 5D and 10D. The American ASME B16.9 uses the terms Long Radius and Short Radius: Long Radius roughly corresponds to 3D, Short Radius roughly to 2D.
Still, the standards differ in places. A pipe bend with an outside diameter of 101.6 mm has a bending diameter of 190.0 mm as type 2D to EN 10253-2:2008 – but only 177.8 mm as Short Radius to ASME B16.9. As type 5D the bending diameter is 415.0 mm to EN 10253-2:2008, but 410 mm to EN 10253-4 (for austenitic steels). Care is needed here to avoid mix-ups.
Type 2D – tight bending radius
Type 2D pipe bends have a tight bending radius approximately equal to one pipe diameter. They allow compact changes of direction where space is limited and are geometrically comparable to short-radius elbows to ASME B16.9. When made as Type B to EN 10253-2, an increased wall thickness is required, particularly on the intrados (inside of the bend), to ensure full internal pressure resistance.
Many applications need pipe bends with tighter tolerances on the bending diameter – and that is where Siekmann comes in: our manufacturing processes achieve much tighter tolerances than the standard values. On request, instead of the ±7 mm of EN 10253-2, we can also manufacture pipe bends with a tolerance of down to ±1 mm on the bending radius.
Types 2D, 3D and 5D compared across standards
The table below compares the bending radii of the types across the different editions of the standards (without guarantee). The “EN 10253-2 2021-11” columns already show the new 2021 edition; for EN 10253-4, DIN EN 10253-4:2025-10 has applied since October 2025 with further changes to the bending radii – we are happy to advise you.
| OD mm | 2D EN 10253-2:2021 | 2D EN 10253-2:2008 | 2D EN 10253-4:2008 | 3D EN 10253-2:2021 | 3D EN 10253-2:2008 | 3D EN 10253-4:2008 | 5D EN 10253-2:2021 | 5D EN 10253-2:2008 | 5D EN 10253-4:2008 |
|---|---|---|---|---|---|---|---|---|---|
| 17.2 | – | – | – | – | – | – | – | – | – |
| 20.0 | – | – | – | – | – | – | – | – | – |
| 21.3 | 17.5 | 25.0 | 25.0 | 28.0 | 38.0 | 28.0 | 42.5 | 42.5 | 45.0 |
| 25.0 | – | – | – | 27.5 | – | – | – | – | – |
| 26.9 | 25.0 | 25.0 | 25.0 | 29.0 | 38.0 | 29.0 | 57.5 | 57.5 | 57.0 |
| 30.0 | – | – | – | – | – | – | – | – | – |
| 31.8 | – | – | – | 35.0 | – | – | – | – | – |
| 33.7 | 25.0 | 25.0 | 28.0 | 38.0 | 38.0 | 38.0 | 72.5 | 72.5 | 72.0 |
| 35.0 | – | – | – | – | – | – | – | – | – |
| 38.0 | 32.5 | – | – | 45.0 | 45.0 | – | 82.5 | 82.5 | – |
| 42.4 | 32.0 | 32.0 | 32.0 | 48.0 | 48.0 | 48.0 | 92.5 | 92.5 | 93.0 |
| 44.5 | – | – | – | – | – | – | – | – | – |
| 48.3 | 38.0 | 38.0 | 38.0 | 57.0 | 57.0 | 57.0 | 107.5 | 109.5 | 108.0 |
| 51.0 | 45.0 | – | – | 63.0 | 63.0 | – | 115.0 | 122.5 | – |
| 54.0 | – | – | – | – | – | – | – | – | – |
| 57.0 | 52.5 | – | – | 72.0 | 72.0 | – | 127.5 | 130.0 | – |
| 60.3 | 51.0 | 51.0 | 51.0 | 76.0 | 76.0 | 76.0 | 135.0 | 137.5 | 135.0 |
| 63.5 | 57.5 | – | – | 82.5 | – | – | 142.5 | – | – |
| 70.0 | 65.0 | – | – | 92.0 | 92.0 | – | 160.0 | 160.0 | – |
| 76.1 | 63.0 | 63.0 | 63.0 | 95.0 | 95.0 | 95.0 | 175.0 | 175.0 | 175.0 |
| 82.5 | 77.5 | – | – | 107.5 | – | – | 190.0 | – | – |
| 88.9 | 76.0 | 76.0 | 76.0 | 114.0 | 114.0 | 114.0 | 205.0 | 207.5 | 205.0 |
| 95.0 | – | – | – | – | – | – | – | – | – |
| 101.6 | 95.0 | – | – | 133.0 | 133.0 | – | 237.5 | 235.0 | – |
| 108.0 | 100.0 | – | – | 142.5 | 142.5 | – | 253.0 | 253.0 | – |
| 114.3 | 102.0 | 102.0 | 102.0 | 152.0 | 152.0 | 152.0 | 270.0 | 270.0 | 270.0 |
| 121.0 | – | – | – | – | – | – | – | – | – |
| 127.0 | – | – | – | 175.0 | – | – | – | – | – |
| 133.0 | 125.0 | – | – | 181.0 | 181.0 | – | 312.5 | 311.5 | – |
| 139.7 | 127.0 | 127.0 | 127.0 | 190.0 | 190.0 | 190.0 | 330.0 | 330.0 | 330.0 |
| 146.0 | – | – | – | – | – | – | – | – | – |
| 152.4 | – | – | – | 215.0 | – | – | – | – | – |
| 159.0 | 150.0 | – | – | 216.0 | 216.0 | – | 375.0 | 375.0 | – |
| 165.1 | – | – | – | – | – | – | – | – | – |
| 168.3 | 152.0 | 152.0 | 152.0 | 229.0 | 229.0 | 229.0 | 390.0 | 390.0 | 390.0 |
| 177.8 | – | – | – | 250.0 | – | – | – | – | – |
| 193.7 | 180.0 | – | – | 270.0 | 270.0 | – | – | – | – |
| 219.1 | 203.0 | 203.0 | 203.0 | 305.0 | 305.0 | 305.0 | 510.0 | 515.0 | 510.0 |
Bending radii
Which bending radii does Siekmann offer?
We also manufacture pipe bends outside the standard radii 2D, 3D and 5D. Our extensive range of tools allows many special sizes up to 219 mm outside diameter. The table below lists every bending radius we have already produced pipe bends with.
| Outside diameter mm | Bending radius R mm |
|---|---|
| 10 | 20 |
| 14 | 20 |
| 16 | 16 |
| 18 | 21 |
| 20 | 16 – 25 – 26.5 |
| 21.3 | 17.5 – 19.5 – 25 – 27.5 – 28 – 38 – 42.5 – 43.5 – 150 |
| 22 | 38 – 45 – 110 |
| 25 | 21 – 25 – 27.5 – 30 – 34 – 44 – 45 – 53 – 60 – 90 |
| 26.9 | 24 – 25 – 25.5 – 28.75 – 29 – 30 – 32 – 34 – 38 – 39 – 40 – 42.5 – 47.5 – 50 – 52.5 – 57.5 – 58.5 – 67.5 – 70 – 85 – 100 – 190 |
| 28 | 28.5 – 32.5 – 33.5 – 35 – 42 – 48 |
| 30 | 25 – 29 – 33.5 – 34 – 35 – 37.5 – 45 – 50 – 55 – 62.5 – 68 |
| 31.8 | 24 – 25 – 27.5 – 30 – 32.5 – 35 – 35.5 – 36.5 – 38 – 39 – 40 – 45 – 50 – 55 – 60 – 63.5 – 67.5 – 80 – 100 – 105 – 112.5 |
| 32 | 25 – 28 – 32.5 |
| 33.7 | 22.5 – 25 – 26.5 – 28 – 30 – 31.5 – 35 – 37.5 – 38 – 39.5 – 40 – 45 – 50 – 60 – 72.5 – 125 – 135 – 240 |
| 35 | 25.5 – 38 – 45 – 45 – 46.5 – 60 – 75 – 100 |
| 38 | 25 – 27 – 27.5 – 29.5 – 30 – 32 – 32.5 – 35 – 37.5 – 37.75 – 38 – 38.5 – 39.5 – 40 – 40.5 – 42.5 – 45 – 45.5 – 46.5 – 47.5 – 48 – 50 – 51.3 – 55 – 57 – 57.5 – 59 – 60 – 65 – 66.5 – 70 – 75 – 80 – 82.5 – 83 – 85 – 93 – 99 – 113 – 145 – 190 |
| 40 | 47.5 – 51.5 – 55 – 185 |
| 42.4 | 30 – 31 – 32 – 37.5 – 38.5 – 42.5 – 45 – 46 – 48 – 49 – 50 – 57 – 63 – 65 – 70 – 72.5 – 75 – 80 – 92.5 – 93.5 – 185 |
| 44.5 | 34 – 35 – 40 – 42.25 – 45 – 50 – 51 – 52.5 – 53.5 – 55 – 55.5 – 57.5 – 70 – 70.5 – 80 – 97.5 – 99.5 – 136 |
| 48.3 | 38 – 39 – 40 – 42.5 – 45.5 – 48 – 50 – 51 – 57 – 60 – 75 – 76.2 – 80 – 85 – 100 – 107.5 – 109.5 – 112.5 – 115 – 135 – 249 |
| 51 | 32.5 – 38 – 45 – 46.5 – 47.5 – 51 – 52.5 – 55 – 57 – 61 – 63.5 – 65 – 67.5 – 69.85 – 76.2 – 80 – 92.5 – 115 – 122.5 |
| 54 | 50 – 54 – 72.5 – 97.5 |
| 57 | 42.5 – 52.5 – 53.5 – 57.5 – 66 – 72 – 75 – 77.5 – 84 – 85 – 90 – 92.5 – 102.5 – 104 – 112.5 – 127.5 |
| 60.3 | 38.1 – 40 – 48.75 – 51 – 55 – 57.15 – 60 – 66 – 75 – 76 – 77.5 – 78.5 – 84 – 90 – 95 – 100 – 101.5 – 107.5 – 109 – 117 – 122 – 135 – 140 – 240 – 250 – 350 – 400 |
| 63.5 | 41.25 – 46.5 – 55 – 57.5 – 59 – 64 – 77.5 – 82.5 – 115 – 142.5 – 210 |
| 70 | 50 – 55 – 62.5 – 65 – 75 – 80.5 – 92 – 94 – 95 – 127.5 – 161.5 – 165 |
| 73 | 63.5 – 77.5 |
| 75 | 95 |
| 76.1 | 63 – 70 – 77 – 87.5 – 88 – 95 – 97 – 95 – 105 – 137 – 140 – 140.5 – 150 – 175 |
| 80 | 78.5 – 109 – 160 |
| 82.5 | 63.5 – 77.5 – 79 – 80 – 107.5 – 114.5 – 175 – 190 |
| 85 | 116.5 |
| 88.9 | 57.5 – 58 – 76 – 78 – 80 – 82.5 – 87.5 – 114 – 162.5 – 165 – 185 – 205 |
| 100 | 133 |
| 101.6 | 76 – 89 – 95 – 97 – 133.5 – 150 – 180 – 190 – 237.5 |
| 102 | 126 – 250 |
| 106 | 144.5 |
| 108 | 100 – 101.5 – 142.5 – 200 – 250 – 252.5 |
| 114.3 | 102 – 105 – 116 – 135 – 152 – 220 – 270 |
| 121 | 112.5 – 120 – 152 – 170 – 175 – 282 |
| 127 | 107.5 – 117.5 – 138.5 – 175 – 235 – 300 |
| 133 | 125 – 181 – 250 – 312.5 |
| 139.7 | 127 – 132.5* – 190 – 250* – 270* – 330* |
| 152 | 142.5* – 215* |
| 159 | 150* – 216* |
| 168.3 | 152* – 229* – 390* |
| 177.8 | 250* |
| 193.7 | 270* |
| 219.1 | 203* – 305* |
* only possible at 90°
Your bending radius is not listed? Feel free to ask about other radii.
Ask about a radius →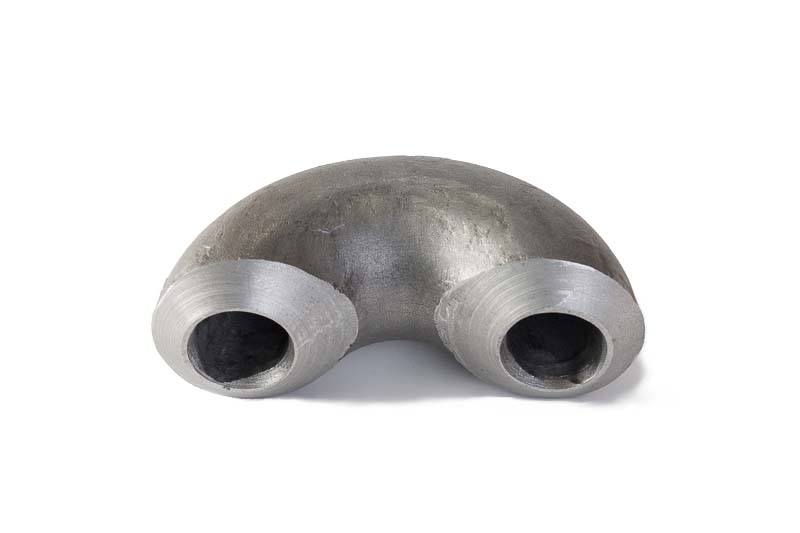
Company
Siekmann GmbH & Co. KG – manufacturer of special pipe bends
Founded as a forge in 1907, we have been making pipe bends since 1940 – and today we specialise in special pipe bends made from seamless pipe.
Newly developed production processes, experienced staff and constant checks at every stage of manufacture ensure the highest quality.
- Special sizes – also outside standard dimensions
- Manufacture of heavy-wall pipe bends
- Small batches too
- Wide range of materials – carbon steel / stainless steel
- Very short delivery times
- Pipe bends with tight tolerances
Our aim is to supply pipe bends quickly, reliably and in the highest quality. A large selection of tools allows us to produce almost any pipe bend between 13.7 mm and 219.1 mm outside diameter – especially with heavy walls.
Get to know us and get in touch – please use our request form for enquiries. You will find your sales contacts on the contact page.
History
- 1907Founded as a village forge – forged parts for local agriculture
- 1928First products for the heating sector
- 1940The first pipe bends are successfully produced
- 1957New production site in Lohne
- 1970First trials with heavy-wall pipe bends
- 1992Production switched to heavy-wall special pipe bends – newly developed manufacturing processes form the basis of today’s success
- todayAcquisition of new land and construction of a new production hall
References
In use worldwide
Our pipe bends are in use worldwide – including at:
- Total S.A.
- Siemens
- Hitachi Power
- Alstom Power
- Exxon Mobil Production
- Buhlmann Rohr-Fittings-Stahlhandel
- STAROFIT Klose GmbH & Co. KG
- ThyssenKrupp Schulte GmbH
- RFF Rohr Flansch Fittings Handels GmbH
- Oschatz GmbH
- BHR Engineering & Construction
- Piping-Service Steuer Handelsges. mbH
Request pipe bends
Send us size, material, standard and quantity – we will get back to you quickly with a quote.